APO RESEARCH · REPORT
Knife Gate Valves
Knife gate valves translate a blade across the flow passage. Blade, body and seat construction determine how the valve closes through a solids-bearing stream.
Product & engineering
Understand the product.
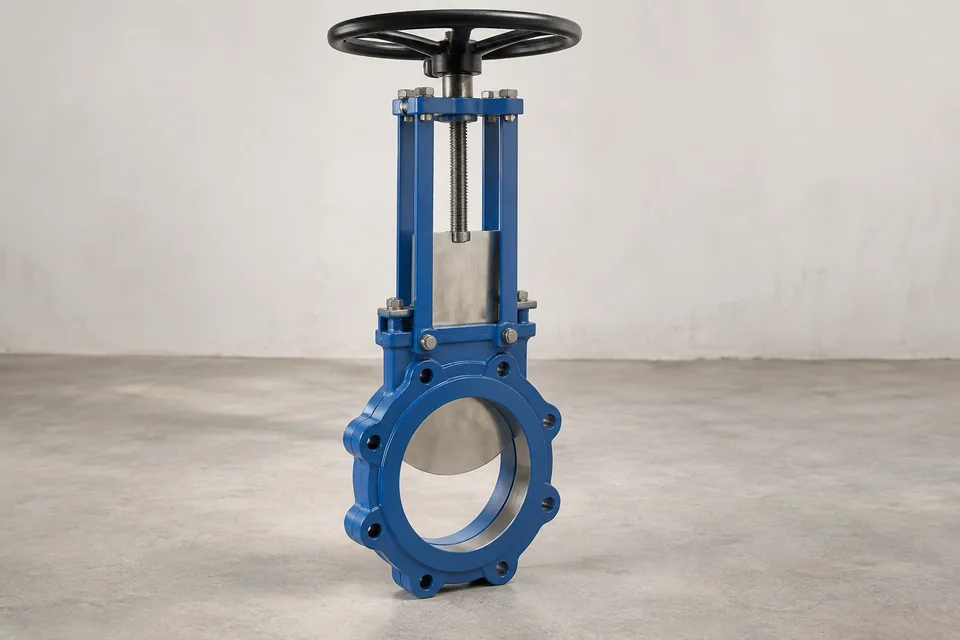
A knife gate valve is a linear-isolation valve engineered to cut through and seal against media with a high solids load—fibrous pulps, slurries, viscous pastes, and wastewater with entrained debris—where conventional wedge gates, globes, or butterflies are prone to clogging or accelerated wear. The defining element is a flat, sharpened gate that travels perpendicular to the flow and shears accumulated solids as it enters a guided seat pocket. In its simplest, bonnetless form the valve body is a short-pattern wafer or lug casting with full-bore geometry to minimize pressure drop; the gate slides between replaceable seats and a packing chamber isolates the stem from the process. Closing force is delivered through a stem-and-yoke mechanism or an actuator sized for the required differential pressure and frictional loads. Properly engineered, the design provides tight shutoff in low-to-moderate pressure services with exceptional tolerance for suspended solids.
From a construction standpoint, the fundamental structure comprises a body (cast or fabricated), a gate with a beveled cutting edge, seat/liner elements that establish shutoff, guides and chest scrapers that maintain alignment and keep debris away from packing, a packing chamber with gland follower and studs, and a yoke or topworks that carries stem thrust into the gate. Stems are typically precision-machined stainless with ACME or trapezoidal threads to transmit high linear force with moderate torque; rising-stem patterns provide direct position indication, while non-rising stems minimize topclearance. For ergonomic or space reasons, handwheels may be replaced by bevel-gear operators, chainwheels, or compact gearboxes that de-multiply torque and improve seating consistency.
Two flow-direction philosophies are common. Unidirectional valves use a seat profile and downstream cavity that the gate wedges into; they deliver very low leakage in the preferred direction with compact construction, but rely on correct orientation and backpressure limits. Bidirectional valves employ opposing seats (often energized elastomer or contained lip designs) to achieve shutoff in either direction, preventing cavity buildup and simplifying installation where piping layouts or transient conditions reverse flow. For highly abrasive duties, “O-port” gates with a round through-hole or guided “through-gate” geometries maintain a continuous bore during throttled travel and reduce jamming, at the expense of weight and actuation force.
Materials and sealing systems are selected around corrosion, temperature, and abrasion. Bodies are commonly 304/316 stainless for pulp, FGD, or wastewater; duplex stainless, alloy 20, or nickel alloys protect against chloride stress-corrosion or acidic slurries; ductile iron offers economy for neutral services; and heavy-duty variants add wear sleeves or hardfacing in the seat zone. Gates use hardened stainless with beveled edges to shear fibers; severe abrasion service may specify Stellite or tungsten-carbide overlays. Seat options span resilient elastomers (EPDM, NBR, natural rubber, neoprene) for bubble-tight shutoff at low pressures, PTFE-based seats for chemical resistance, and metal-seated designs where temperature, vacuum, or cutting action would damage polymers. Packing systems range from PTFE/graphite to braided fibers with lantern rings and purge ports; live-loading maintains compression through thermal and pressure cycles. Where fugitive emissions or safety matter, enclosed bonnets or dust boots prevent discharge to atmosphere when the gate is withdrawn.
Manufacturing processes reflect service severity and size. Small to mid sizes often use sand-cast or investment-cast bodies followed by CNC machining of guides, seat pockets, and gasket faces to tight flatness and perpendicularity. Large diameters are frequently fabricated from rolled plate and bar with full-penetration welds; critical welds are dye-penetrant tested and stress-relieved as required. Elastomer seats are compression-molded and bonded into retainers or liners; rubber-lined bodies are vulcanized to achieve adhesion and wear resistance. Hardfacing is applied by PTA, HVOF, or weld-overlay in high-wear zones. After assembly, valves undergo shell and seat testing, torque/force calibration, and where specified, surface treatments such as epoxy-phenolic coatings, passivation of stainless, and fastener protection to ISO/ASTM practice.
Core technologies that differentiate performance include energised lip-seats that maintain sealing load as the gate traverses accumulated solids; full-bore liners that decouple erosion from the pressure boundary; scrapers and chest deflectors that keep fibers and grit away from packing; purge ports and flush rings that hydro-clean seat pockets; and O-port gates that present a continuous aperture to abrasive slurries. In viscous or settling duty, bottom-entry cleanouts, deflector cones, and guided gate shoes materially reduce jamming and seat scouring. For odor or toxicity control, bonneted designs with venting and purge manifolds uphold environmental compliance without compromising maintainability.
End connections reflect installation constraints and isolation needs. Wafer bodies minimize weight and face-to-face length; lug bodies with threaded inserts enable true dead-end service when properly rated and blind-flanged; full-flanged bodies simplify alignment on large diameters. Some heavy-duty mining designs incorporate retainable wear rings and replaceable flanged spools to restore face-to-face after refurbishment. Typical pressure classes are in the ASME Class 150 / PN10–PN16 range with larger diameters trending lower due to seat loads, though specialty designs reach higher ratings in mining or power applications. Size coverage commonly extends from DN50/NPS 2 up to DN1200–DN2000 in fabricated constructions, with full-port openings to pass large particles. Temperature capability is governed by soft-goods and coating systems; elastomer-seated valves are typically limited to ~100–120 °C, PTFE/graphite packings elevate this, and metal-seated, bonneted builds can extend further.
Actuation and automation are integral to reliability. Manual handwheel with rising or non-rising stems works for clean, low-cycle services. Pneumatic cylinders (double-acting or spring-return) are preferred for fast, repetitive strokes in wastewater, pulp, and bulk solids handling; hydraulic actuation delivers compact high thrust where ΔP is large or media is sticky; electric multi-turn or linear actuators suit remote plants with limited air infrastructure. Controls often add position indication, limit switches, solenoid valves, air sets, and smart positioners when the valve is used for coarse throttling—though knife gates are first and foremost isolation devices, and any control duty should respect the valve’s trim, ΔP, and vibration limits to avoid accelerated seat wear. For safety instrumented functions, actuators can be specified with defined fail-positions, quick-exhaust circuits, partial-stroke testing, and SIL-rated accessories; signal interfaces range from dry contacts to analog, fieldbus, and digital diagnostics that support predictive maintenance.
Performance is evaluated across shutoff tightness, pressure/temperature envelope, solids-handling capability, and actuation repeatability. Resilient-seated valves often warrant “bubble-tight” isolation at rated pressure in the preferred direction, while metal-seated trims specify calibrated leakage consistent with ISO 5208 or EN 12266-1 categories. Flow capacity follows the full-port geometry and can be represented by Kv/Cv data for sizing upstream blowers or pumps, with the caveat that knife gates should not be used as fine control elements at high ΔP where cavitation or vibration can damage seats and guides. Cycle life depends on solids hardness, velocity, and seat material; specifying sacrificial liners and oversizing actuators for worst-case friction lowers force spikes at closure and extends service intervals.
Engineering and selection hinge on a small set of critical variables: solids loading (% by volume), particle size and hardness, viscosity, pH/chemistry, required leakage class, differential pressure at closure, cycling frequency, and cleaning strategy. Abrasive slurries push designs toward full-bore ports, robust gate guides, elastomer liners or replaceable wear rings, purgeable packing, and deflector cones that shield the seat pocket. Fibrous stock demands sharp, self-cleaning gates and flush ports to evacuate the cavity. For hazardous or odorous services, bonneted construction with zero-leakage packing and top-works seals is increasingly specified. When dead-end isolation is required, confirm the valve’s unbraced side rating and the need for a downstream blind. Hydrostatic testing typically follows MSS and ISO conventions—shell tests at 1.5× rating and seat tests at ~1.1×—with leakage rates per ISO 5208 or manufacturer commitments. Dimensional interfaces align to EN 1092-1 or ASME B16.5 for flanges; design and service practice reference MSS-SP-81 for stainless, bonnetless knife gates, with additional guidance from MSS specifications on bonneted variants and packing.
Installation and use benefit from a few disciplined practices. Orient unidirectional valves correctly with respect to pressure and solids flow; provide adequate upstream and downstream straight runs to minimize turbulence that can drive uneven seat wear; use full-face gaskets compatible with liner materials to avoid cold-flow or chemical attack; tighten flange bolts in star patterns to specified torque and re-torque after initial thermal cycles; support the valve weight independently of pipe to avoid flange distortion; and, where settling is expected, include low-point drains or purge taps for periodic flushing. Commissioning should verify actuator end-stop settings, limit switch calibration, and that available thrust comfortably exceeds worst-case friction plus ΔP forces without stalling.
Lifecycle cost is driven less by initial price than by seat and packing longevity, ease of maintenance, and unplanned downtime. Design details like external chest scrapers, dust boots, accessible packing glands, split bodies for in-line seat replacement, and purge ports materially reduce cleaning and rebuild time. In abrasive circuits, specifying sacrificial liners concentrates wear into low-cost components; in corrosive duty, upgrading a few wetted parts (gate, seats, fasteners) often outperforms wholesale alloy upgrades. Actuator sizing with adequate safety factors prevents mid-stroke stalls that damage seats and gates. Predictive maintenance—tracking cycle counts, actuator current, and seat leakage trends—allows planned overhauls before loss of isolation impacts upstream processes. A practical maintenance plan includes periodic packing adjustments, scheduled liner/seat inspections based on solids hardness and velocity, and a spares kit comprising packing rings, seat/liner, stem nut, guide shoes, and actuator seals to compress turnaround windows.
Application domains illustrate the knife gate’s value proposition. In pulp and paper, valves isolate stock lines, bleach plants, and rejects handling without fiber bridging. In mining and mineral processing, they handle tailings, cyclone underflow, and thickener underflow where particle abrasion and settling are severe. Municipal and industrial wastewater plants rely on them for grit, sludge, and scum services where rags and debris challenge other trims. Power and FGD systems exploit corrosion-resistant, rubber-lined bodies to manage limestone slurries and gypsum. Food, bio-process, and fine chemicals adopt clean-in-place friendly designs with polished wetted parts and FDA-compliant elastomers where sanitary isolation—not throttling—is required. Across all, knife gates excel when the medium will foul, pack, or erode more delicate valve internals.
From a regulatory and conformity standpoint, manufacturers align pressure-bearing parts to the European Pressure Equipment Directive (PED) or UKCA where applicable; potable-water service may require NSF/ANSI/CAN 61 or analogous regional approvals; hazardous areas drive actuator and limit-switch selections to ATEX/IECEx or North American Class/Division standards. Corrosive sour environments reference material selection per NACE MR0175/ISO 15156. Testing and acceptance commonly reference ISO 5208 or EN 12266-1 for seat and shell tightness, with dimensional interfaces per ASME B16.5 and EN 1092-1; MSS-SP-81 provides design practice for stainless bonnetless knife gate valves, and project documentation packages increasingly demand MTR traceability, hydrotest records, coating data sheets, and emissions declarations for packing systems.
Investors evaluating the segment should recognize the defensibility of application know-how and aftermarket content. While base bodies are relatively standardized, performance in difficult slurries depends on proprietary seat geometries, purge schemes, coatings, and gate treatments validated over thousands of cycles in specific industries. Actuation/controls integration, engineered-to-order large diameters, and rebuild kits generate attractive service revenue, and switching costs are non-trivial once a plant standardizes on a platform. Secular demand is tied to water and wastewater infrastructure, mining and tailings stewardship, pulp and packaging growth, and emissions-control retrofits—each favoring reliable isolation in dirty service over high-precision control.
Limitations are equally important to set expectations. Knife gate valves are not optimized for high-pressure gases or critical throttling where cavitation and vibration dominate; they are fundamentally isolation devices with modest pressure ratings, and misapplication leads to rapid seat and gate degradation. Bonnetless patterns will vent to atmosphere as the gate withdraws, which is unacceptable for toxic, volatile, or hygienic streams without enclosures. Ensuring correct orientation for unidirectional valves, respecting dead-end ratings, and sizing actuators for worst-case ΔP are non-negotiable engineering disciplines.
In summary, a knife gate valve is a purpose-built isolation solution for solids-laden, viscous, or fibrous media. Its value comes from a shearing gate, maintainable seat and packing systems, and construction tailored to abrasion and corrosion risks. When specified with clear knowledge of the process chemistry, solids profile, and operating envelope—and supported by appropriate actuation, installation discipline, and maintenance practices—it delivers low-leakage isolation, high availability, and predictable lifecycle costs in services where many other valve types struggle.
Solids size, concentration and abrasion influence seat and blade requirements. A general knife gate and a push-through slurry valve have different handling arrangements. Products intended for on-off isolation should not automatically be used for throttling.
What turns activity into demand
The purchase addresses both flow isolation and the material left around the blade. Wear and displaced solids connect the installed base to replacement parts. Separate complete valves, actuation, replacement sleeves and flushing arrangements. Do not equate every knife gate with the same slurry capability.
The commercial boundary
Separate complete valves, actuation, replacement sleeves and flushing arrangements. Do not equate every knife gate with the same slurry capability.
Technical reading
Selected research
Market Structure
Global Knife Gate Valves Market by Size, by Type, by Application, by Region, History and Forecast 2021-2032
Market perspective
A knife gate valve is a linear-isolation valve engineered to cut through and seal against media with a high solids load—fibrous pulps, slurries, viscous pastes, and wastewater with entrained debris—where conventional wedge gates, globes, or butterflies are prone to clogging or accelerated wear. The defining element is a flat, sharpened gate that travels perpendicular to the flow and shears accumulated solids as it enters a guided seat pocket. In its simplest, bonnetless form the valve body is a short-pattern wafer or lug casting with full-bore geometry to minimize pressure drop; the gate slides between replaceable seats and a packing chamber isolates the stem from the process. Closing force is delivered through a stem-and-yoke mechanism or an actuator sized for the required differential pressure and frictional loads. Properly engineered, the design provides tight shutoff in low-to-moderate pressure services with exceptional tolerance for suspended solids.
From a construction standpoint, the fundamental structure comprises a body (cast or fabricated), a gate with a beveled cutting edge, seat/liner elements that establish shutoff, guides and chest scrapers that maintain alignment and keep debris away from packing, a packing chamber with gland follower and studs, and a yoke or topworks that carries stem thrust into the gate. Stems are typically precision-machined stainless with ACME or trapezoidal threads to transmit high linear force with moderate torque; rising-stem patterns provide direct position indication, while non-rising stems minimize topclearance. For ergonomic or space reasons, handwheels may be replaced by bevel-gear operators, chainwheels, or compact gearboxes that de-multiply torque and improve seating consistency.
Two flow-direction philosophies are common. Unidirectional valves use a seat profile and downstream cavity that the gate wedges into; they deliver very low leakage in the preferred direction with compact construction, but rely on correct orientation and backpressure limits. Bidirectional valves employ opposing seats (often energized elastomer or contained lip designs) to achieve shutoff in either direction, preventing cavity buildup and simplifying installation where piping layouts or transient conditions reverse flow. For highly abrasive duties, “O-port” gates with a round through-hole or guided “through-gate” geometries maintain a continuous bore during throttled travel and reduce jamming, at the expense of weight and actuation force.
Read the full market overview
Materials and sealing systems are selected around corrosion, temperature, and abrasion. Bodies are commonly 304/316 stainless for pulp, FGD, or wastewater; duplex stainless, alloy 20, or nickel alloys protect against chloride stress-corrosion or acidic slurries; ductile iron offers economy for neutral services; and heavy-duty variants add wear sleeves or hardfacing in the seat zone. Gates use hardened stainless with beveled edges to shear fibers; severe abrasion service may specify Stellite or tungsten-carbide overlays. Seat options span resilient elastomers (EPDM, NBR, natural rubber, neoprene) for bubble-tight shutoff at low pressures, PTFE-based seats for chemical resistance, and metal-seated designs where temperature, vacuum, or cutting action would damage polymers. Packing systems range from PTFE/graphite to braided fibers with lantern rings and purge ports; live-loading maintains compression through thermal and pressure cycles. Where fugitive emissions or safety matter, enclosed bonnets or dust boots prevent discharge to atmosphere when the gate is withdrawn.
Manufacturing processes reflect service severity and size. Small to mid sizes often use sand-cast or investment-cast bodies followed by CNC machining of guides, seat pockets, and gasket faces to tight flatness and perpendicularity. Large diameters are frequently fabricated from rolled plate and bar with full-penetration welds; critical welds are dye-penetrant tested and stress-relieved as required. Elastomer seats are compression-molded and bonded into retainers or liners; rubber-lined bodies are vulcanized to achieve adhesion and wear resistance. Hardfacing is applied by PTA, HVOF, or weld-overlay in high-wear zones. After assembly, valves undergo shell and seat testing, torque/force calibration, and where specified, surface treatments such as epoxy-phenolic coatings, passivation of stainless, and fastener protection to ISO/ASTM practice.
Core technologies that differentiate performance include energised lip-seats that maintain sealing load as the gate traverses accumulated solids; full-bore liners that decouple erosion from the pressure boundary; scrapers and chest deflectors that keep fibers and grit away from packing; purge ports and flush rings that hydro-clean seat pockets; and O-port gates that present a continuous aperture to abrasive slurries. In viscous or settling duty, bottom-entry cleanouts, deflector cones, and guided gate shoes materially reduce jamming and seat scouring. For odor or toxicity control, bonneted designs with venting and purge manifolds uphold environmental compliance without compromising maintainability.
End connections reflect installation constraints and isolation needs. Wafer bodies minimize weight and face-to-face length; lug bodies with threaded inserts enable true dead-end service when properly rated and blind-flanged; full-flanged bodies simplify alignment on large diameters. Some heavy-duty mining designs incorporate retainable wear rings and replaceable flanged spools to restore face-to-face after refurbishment. Typical pressure classes are in the ASME Class 150 / PN10–PN16 range with larger diameters trending lower due to seat loads, though specialty designs reach higher ratings in mining or power applications. Size coverage commonly extends from DN50/NPS 2 up to DN1200–DN2000 in fabricated constructions, with full-port openings to pass large particles. Temperature capability is governed by soft-goods and coating systems; elastomer-seated valves are typically limited to ~100–120 °C, PTFE/graphite packings elevate this, and metal-seated, bonneted builds can extend further.
Actuation and automation are integral to reliability. Manual handwheel with rising or non-rising stems works for clean, low-cycle services. Pneumatic cylinders (double-acting or spring-return) are preferred for fast, repetitive strokes in wastewater, pulp, and bulk solids handling; hydraulic actuation delivers compact high thrust where ΔP is large or media is sticky; electric multi-turn or linear actuators suit remote plants with limited air infrastructure. Controls often add position indication, limit switches, solenoid valves, air sets, and smart positioners when the valve is used for coarse throttling—though knife gates are first and foremost isolation devices, and any control duty should respect the valve’s trim, ΔP, and vibration limits to avoid accelerated seat wear. For safety instrumented functions, actuators can be specified with defined fail-positions, quick-exhaust circuits, partial-stroke testing, and SIL-rated accessories; signal interfaces range from dry contacts to analog, fieldbus, and digital diagnostics that support predictive maintenance.
Performance is evaluated across shutoff tightness, pressure/temperature envelope, solids-handling capability, and actuation repeatability. Resilient-seated valves often warrant “bubble-tight” isolation at rated pressure in the preferred direction, while metal-seated trims specify calibrated leakage consistent with ISO 5208 or EN 12266-1 categories. Flow capacity follows the full-port geometry and can be represented by Kv/Cv data for sizing upstream blowers or pumps, with the caveat that knife gates should not be used as fine control elements at high ΔP where cavitation or vibration can damage seats and guides. Cycle life depends on solids hardness, velocity, and seat material; specifying sacrificial liners and oversizing actuators for worst-case friction lowers force spikes at closure and extends service intervals.
Engineering and selection hinge on a small set of critical variables: solids loading (% by volume), particle size and hardness, viscosity, pH/chemistry, required leakage class, differential pressure at closure, cycling frequency, and cleaning strategy. Abrasive slurries push designs toward full-bore ports, robust gate guides, elastomer liners or replaceable wear rings, purgeable packing, and deflector cones that shield the seat pocket. Fibrous stock demands sharp, self-cleaning gates and flush ports to evacuate the cavity. For hazardous or odorous services, bonneted construction with zero-leakage packing and top-works seals is increasingly specified. When dead-end isolation is required, confirm the valve’s unbraced side rating and the need for a downstream blind. Hydrostatic testing typically follows MSS and ISO conventions—shell tests at 1.5× rating and seat tests at ~1.1×—with leakage rates per ISO 5208 or manufacturer commitments. Dimensional interfaces align to EN 1092-1 or ASME B16.5 for flanges; design and service practice reference MSS-SP-81 for stainless, bonnetless knife gates, with additional guidance from MSS specifications on bonneted variants and packing.
Installation and use benefit from a few disciplined practices. Orient unidirectional valves correctly with respect to pressure and solids flow; provide adequate upstream and downstream straight runs to minimize turbulence that can drive uneven seat wear; use full-face gaskets compatible with liner materials to avoid cold-flow or chemical attack; tighten flange bolts in star patterns to specified torque and re-torque after initial thermal cycles; support the valve weight independently of pipe to avoid flange distortion; and, where settling is expected, include low-point drains or purge taps for periodic flushing. Commissioning should verify actuator end-stop settings, limit switch calibration, and that available thrust comfortably exceeds worst-case friction plus ΔP forces without stalling.
Lifecycle cost is driven less by initial price than by seat and packing longevity, ease of maintenance, and unplanned downtime. Design details like external chest scrapers, dust boots, accessible packing glands, split bodies for in-line seat replacement, and purge ports materially reduce cleaning and rebuild time. In abrasive circuits, specifying sacrificial liners concentrates wear into low-cost components; in corrosive duty, upgrading a few wetted parts (gate, seats, fasteners) often outperforms wholesale alloy upgrades. Actuator sizing with adequate safety factors prevents mid-stroke stalls that damage seats and gates. Predictive maintenance—tracking cycle counts, actuator current, and seat leakage trends—allows planned overhauls before loss of isolation impacts upstream processes. A practical maintenance plan includes periodic packing adjustments, scheduled liner/seat inspections based on solids hardness and velocity, and a spares kit comprising packing rings, seat/liner, stem nut, guide shoes, and actuator seals to compress turnaround windows.
Application domains illustrate the knife gate’s value proposition. In pulp and paper, valves isolate stock lines, bleach plants, and rejects handling without fiber bridging. In mining and mineral processing, they handle tailings, cyclone underflow, and thickener underflow where particle abrasion and settling are severe. Municipal and industrial wastewater plants rely on them for grit, sludge, and scum services where rags and debris challenge other trims. Power and FGD systems exploit corrosion-resistant, rubber-lined bodies to manage limestone slurries and gypsum. Food, bio-process, and fine chemicals adopt clean-in-place friendly designs with polished wetted parts and FDA-compliant elastomers where sanitary isolation—not throttling—is required. Across all, knife gates excel when the medium will foul, pack, or erode more delicate valve internals.
From a regulatory and conformity standpoint, manufacturers align pressure-bearing parts to the European Pressure Equipment Directive (PED) or UKCA where applicable; potable-water service may require NSF/ANSI/CAN 61 or analogous regional approvals; hazardous areas drive actuator and limit-switch selections to ATEX/IECEx or North American Class/Division standards. Corrosive sour environments reference material selection per NACE MR0175/ISO 15156. Testing and acceptance commonly reference ISO 5208 or EN 12266-1 for seat and shell tightness, with dimensional interfaces per ASME B16.5 and EN 1092-1; MSS-SP-81 provides design practice for stainless bonnetless knife gate valves, and project documentation packages increasingly demand MTR traceability, hydrotest records, coating data sheets, and emissions declarations for packing systems.
Investors evaluating the segment should recognize the defensibility of application know-how and aftermarket content. While base bodies are relatively standardized, performance in difficult slurries depends on proprietary seat geometries, purge schemes, coatings, and gate treatments validated over thousands of cycles in specific industries. Actuation/controls integration, engineered-to-order large diameters, and rebuild kits generate attractive service revenue, and switching costs are non-trivial once a plant standardizes on a platform. Secular demand is tied to water and wastewater infrastructure, mining and tailings stewardship, pulp and packaging growth, and emissions-control retrofits—each favoring reliable isolation in dirty service over high-precision control.
Limitations are equally important to set expectations. Knife gate valves are not optimized for high-pressure gases or critical throttling where cavitation and vibration dominate; they are fundamentally isolation devices with modest pressure ratings, and misapplication leads to rapid seat and gate degradation. Bonnetless patterns will vent to atmosphere as the gate withdraws, which is unacceptable for toxic, volatile, or hygienic streams without enclosures. Ensuring correct orientation for unidirectional valves, respecting dead-end ratings, and sizing actuators for worst-case ΔP are non-negotiable engineering disciplines.
In summary, a knife gate valve is a purpose-built isolation solution for solids-laden, viscous, or fibrous media. Its value comes from a shearing gate, maintainable seat and packing systems, and construction tailored to abrasion and corrosion risks. When specified with clear knowledge of the process chemistry, solids profile, and operating envelope—and supported by appropriate actuation, installation discipline, and maintenance practices—it delivers low-leakage isolation, high availability, and predictable lifecycle costs in services where many other valve types struggle.
The global Knife Gate Valves market is projected to grow from US$ million in 2026 to US$ million by 2032, implying a CAGR of % over 2026-2032.
The US & Canada market for Knife Gate Valves is projected to increase from US$ million in 2026 to US$ million by 2032, at a CAGR of % over 2026-2032.
The Europe market for Knife Gate Valves is projected to increase from US$ million in 2026 to US$ million by 2032, at a CAGR of % over 2026-2032.
The Asia Pacific market for Knife Gate Valves is projected to increase from US$ million in 2026 to US$ million by 2032, at a CAGR of % over 2026-2032.
The China market for Knife Gate Valves is projected to increase from US$ million in 2026 to US$ million by 2032, at a CAGR of % over 2026-2032.
Leading global manufacturers of Knife Gate Valves include AVK, DeZURIK, Emerson Electric, FLSmidth, ITT, Bray International, Stafsjö Valves, Weir Group and VAG, among others. In 2025, the top three vendors together accounted for approximately % of global revenue.
On the production side, the report examines Knife Gate Valves output, growth rates, and market shares by manufacturer and by region (at regional and country level) for 2021-2026, with forecasts through 2032.
On the consumption side, the report analyzes sales of Knife Gate Valves by region (regional and country level), company, type, and application for 2021-2026 and provides forecasts through 2032.
The report provides an overview of the global Knife Gate Valves market in terms of capacity, output, revenue, and price, analyzing global market trends using historical revenue and sales data for 2021-2025, estimates for 2026, and projected CAGRs through 2032.
The study covers key producers of Knife Gate Valves and consumption patterns in major regions and countries, assesses future market potential, and highlights priority regions and countries for segmenting the market into sub-sectors, with country-specific market value data for the U.S., Canada, Mexico, Brazil, China, Japan, South Korea, Southeast Asia, India, Germany, the U.K., Italy, the Middle East, Africa, and other countries.
The report also presents Knife Gate Valves sales, revenue, market share, and industry ranking for the main manufacturers for 2021-2026, identifies the major stakeholders in the global market, and analyzes their competitive landscape and market positioning based on recent developments and segmental revenues.
In addition, the report analyzes segment data by type and application—covering sales, revenue, and price—for 2021-2032, and evaluates and forecasts the Knife Gate Valves market size, projected growth trends, production technologies, key applications, and end-use industries.
Knife Gate Valves Segment by Company
AVK
DeZURIK
Emerson Electric
FLSmidth
ITT
Bray International
Stafsjö Valves
Weir Group
VAG
Erhard GmbH
WEY Valve
Chisun Valve
GEFA Processtechnik
Zhejiang Linuo Flow
Valmet (Flowrox)
Okumura Engineering
Tecofi
Davis Valve
Supero Seiki
Trueline Valve
Knife Gate Valves Segment by Type
Pneumatic
Electric
Manual
Hydraulic
Knife Gate Valves Segment by Application
Pulp and Paper
Mining
Wastewater Treatment
Chemical Processing
Power Generation
Food & Beverage
Other Industrial Applications
Knife Gate Valves Segment by Region
North America
United States
Canada
Mexico
Europe
Germany
France
U.K.
Italy
Russia
Spain
Netherlands
Switzerland
Sweden
Poland
Asia-Pacific
China
Japan
South Korea
India
Australia
Taiwan
Southeast Asia
South America
Brazil
Argentina
Chile
Middle East & Africa
Egypt
South Africa
Israel
Türkiye
GCC Countries
Study Objectives
1. To analyze and research the global status and future forecast, involving, production, value, consumption, growth rate (CAGR), market share, historical and forecast.
2. To present the key manufacturers, capacity, production, revenue, market share, and Recent Developments.
3. To split the breakdown data by regions, type, manufacturers, and Application.
4. To analyze the global and key regions market potential and advantage, opportunity and challenge, restraints, and risks.
5. To identify significant trends, drivers, influence factors in global and regions.
6. To analyze competitive developments such as expansions, agreements, new product launches, and acquisitions in the market.
Reasons to Buy This Report
1. This report will help the readers to understand the competition within the industries and strategies for the competitive environment to enhance the potential profit. The report also focuses on the competitive landscape of the global Knife Gate Valves market, and introduces in detail the market share, industry ranking, competitor ecosystem, market performance, new product development, operation situation, expansion, and acquisition. etc. of the main players, which helps the readers to identify the main competitors and deeply understand the competition pattern of the market.
2. This report will help stakeholders to understand the global industry status and trends of Knife Gate Valves and provides them with information on key market drivers, restraints, challenges, and opportunities.
3. This report will help stakeholders to understand competitors better and gain more insights to strengthen their position in their businesses. The competitive landscape section includes the market share and rank (in volume and value), competitor ecosystem, new product development, expansion, and acquisition.
4. This report stays updated with novel technology integration, features, and the latest developments in the market.
5. This report helps stakeholders to gain insights into which regions to target globally.
6. This report helps stakeholders to gain insights into the end-user perception concerning the adoption of Knife Gate Valves.
7. This report helps stakeholders to identify some of the key players in the market and understand their valuable contribution.
Chapter Outline
Chapter 1: Provides an overview of the Knife Gate Valves market, including product definition, global market growth prospects, production value, capacity, and average price forecasts (2021-2032).
Chapter 2: Analysis key trends, drivers, challenges, and opportunities within the global Knife Gate Valves industry.
Chapter 3: Detailed analysis of Knife Gate Valves market competition landscape. Including Knife Gate Valves manufacturers' output value, output and average price from 2021 to 2026, as well as competition analysis indicators such as origin, product type, application, merger and acquisition information, etc.
Chapter 4: Provides the analysis of various market segments by type, covering the market size and development potential of each market segment, to help readers find the blue ocean market in different market segments.
Chapter 5: Provides the analysis of various market segments by application, covering the market size and development potential of each market segment, to help readers find the blue ocean market in different downstream markets.
Chapter 6: Provides profiles of key players, introducing the basic situation of the main companies in the market in detail, including product production/output, value, price, gross margin, product introduction, recent development, etc.
Chapter 7: Production/Production Value of Knife Gate Valves by region. It provides a quantitative analysis of the market size and development potential of each region in the next six years.
Chapter 8: Consumption of Knife Gate Valves in regional level and country level. It provides a quantitative analysis of the market size and development potential of each region and its main countries and introduces the market development, future development prospects, market space, and production of each country in the world.
Chapter 9: Analysis of industrial chain, including the upstream and downstream of the industry.
Chapter 10: Concluding Insights of the report.
More report detail
Tables and figures
Scope & coverage.
Types
- Pneumatic
- Electric
- Manual
- Hydraulic
Applications
- Pulp and Paper
- Mining
- Wastewater Treatment
- Chemical Processing
- Power Generation
- Food & Beverage
- Other Industrial Applications
Companies covered
- AVK
- DeZURIK
- Emerson Electric
- FLSmidth
- ITT
- Bray International
- Stafsjö Valves
- Weir Group
- VAG
- Erhard GmbH
- WEY Valve
- Chisun Valve
- GEFA Processtechnik
- Zhejiang Linuo Flow
- Valmet (Flowrox)
- Okumura Engineering
- Tecofi
- Davis Valve
- Supero Seiki
- Trueline Valve
Inside the report.
1 Market Overview
- 1.1 Product Definition
- 1.2 Global Market Growth Prospects
- 1.2.1 Global Knife Gate Valves Production Value Estimates and Forecasts (2021-2032)
- 1.2.2 Global Knife Gate Valves Production Capacity Estimates and Forecasts (2021-2032)
- 1.2.3 Global Knife Gate Valves Production Estimates and Forecasts (2021-2032)
- 1.2.4 Global Knife Gate Valves Market Average Price (2021-2032)
- 1.3 Assumptions and Limitations
- 1.4 Study Goals and Objectives
2 Global Knife Gate Valves Market Dynamics
- 2.1 Knife Gate Valves Industry Trends
- 2.2 Knife Gate Valves Industry Drivers
- 2.3 Knife Gate Valves Industry Opportunities and Challenges
- 2.4 Knife Gate Valves Industry Restraints
3 Knife Gate Valves Market by Manufacturers
- 3.1 Global Knife Gate Valves Production Value by Manufacturers (2021-2026)
- 3.2 Global Knife Gate Valves Production by Manufacturers (2021-2026)
- 3.3 Global Knife Gate Valves Average Price by Manufacturers (2021-2026)
- 3.4 Global Knife Gate Valves Industry Manufacturers Ranking, 2024 VS 2025 VS 2026
- 3.5 Global Knife Gate Valves Key Manufacturers Manufacturing Sites & Headquarters
- 3.6 Global Knife Gate Valves Manufacturers, Product Type & Application
- 3.7 Global Knife Gate Valves Manufacturers Established Date
- 3.8 Market Competitive Analysis
- 3.8.1 Global Knife Gate Valves Market CR5 and HHI
- 3.8.2 Global Top 5 and 10 Knife Gate Valves Players Market Share by Production Value in 2025
- 3.8.3 2025 Knife Gate Valves Tier 1, Tier 2, and Tier 3
4 Knife Gate Valves Market by Type
- 4.1 Knife Gate Valves Type Introduction
- 4.1.1 Pneumatic
- 4.1.2 Electric
- 4.1.3 Manual
- 4.1.4 Hydraulic
- 4.2 Global Knife Gate Valves Production by Type
- 4.2.1 Global Knife Gate Valves Production by Type (2021 VS 2025 VS 2032)
- 4.2.2 Global Knife Gate Valves Production by Type (2021-2032)
- 4.2.3 Global Knife Gate Valves Production Market Share by Type (2021-2032)
- 4.3 Global Knife Gate Valves Production Value by Type
- 4.3.1 Global Knife Gate Valves Production Value by Type (2021 VS 2025 VS 2032)
- 4.3.2 Global Knife Gate Valves Production Value by Type (2021-2032)
- 4.3.3 Global Knife Gate Valves Production Value Market Share by Type (2021-2032)
5 Knife Gate Valves Market by Application
- 5.1 Knife Gate Valves Application Introduction
- 5.1.1 Pulp and Paper
- 5.1.2 Mining
- 5.1.3 Wastewater Treatment
- 5.1.4 Chemical Processing
- 5.1.5 Power Generation
- 5.1.6 Food & Beverage
- 5.1.7 Other Industrial Applications
- 5.2 Global Knife Gate Valves Production by Application
- 5.2.1 Global Knife Gate Valves Production by Application (2021 VS 2025 VS 2032)
- 5.2.2 Global Knife Gate Valves Production by Application (2021-2032)
- 5.2.3 Global Knife Gate Valves Production Market Share by Application (2021-2032)
- 5.3 Global Knife Gate Valves Production Value by Application
- 5.3.1 Global Knife Gate Valves Production Value by Application (2021 VS 2025 VS 2032)
- 5.3.2 Global Knife Gate Valves Production Value by Application (2021-2032)
- 5.3.3 Global Knife Gate Valves Production Value Market Share by Application (2021-2032)
6 Company Profiles
- 6.1 AVK
- 6.1.1 AVK Company Information
- 6.1.2 AVK Business Overview
- 6.1.3 AVK Knife Gate Valves Production, Value and Gross Margin (2021-2026)
- 6.1.4 AVK Knife Gate Valves Product Portfolio
- 6.1.5 AVK Recent Developments
- 6.2 DeZURIK
- 6.2.1 DeZURIK Company Information
- 6.2.2 DeZURIK Business Overview
- 6.2.3 DeZURIK Knife Gate Valves Production, Value and Gross Margin (2021-2026)
- 6.2.4 DeZURIK Knife Gate Valves Product Portfolio
- 6.2.5 DeZURIK Recent Developments
- 6.3 Emerson Electric
- 6.3.1 Emerson Electric Company Information
- 6.3.2 Emerson Electric Business Overview
- 6.3.3 Emerson Electric Knife Gate Valves Production, Value and Gross Margin (2021-2026)
- 6.3.4 Emerson Electric Knife Gate Valves Product Portfolio
- 6.3.5 Emerson Electric Recent Developments
- 6.4 FLSmidth
- 6.4.1 FLSmidth Company Information
- 6.4.2 FLSmidth Business Overview
- 6.4.3 FLSmidth Knife Gate Valves Production, Value and Gross Margin (2021-2026)
- 6.4.4 FLSmidth Knife Gate Valves Product Portfolio
- 6.4.5 FLSmidth Recent Developments
- 6.5 ITT
- 6.5.1 ITT Company Information
- 6.5.2 ITT Business Overview
- 6.5.3 ITT Knife Gate Valves Production, Value and Gross Margin (2021-2026)
- 6.5.4 ITT Knife Gate Valves Product Portfolio
- 6.5.5 ITT Recent Developments
- 6.6 Bray International
- 6.6.1 Bray International Company Information
- 6.6.2 Bray International Business Overview
- 6.6.3 Bray International Knife Gate Valves Production, Value and Gross Margin (2021-2026)
- 6.6.4 Bray International Knife Gate Valves Product Portfolio
- 6.6.5 Bray International Recent Developments
- 6.7 Stafsjö Valves
- 6.7.1 Stafsjö Valves Company Information
- 6.7.2 Stafsjö Valves Business Overview
- 6.7.3 Stafsjö Valves Knife Gate Valves Production, Value and Gross Margin (2021-2026)
- 6.7.4 Stafsjö Valves Knife Gate Valves Product Portfolio
- 6.7.5 Stafsjö Valves Recent Developments
- 6.8 Weir Group
- 6.8.1 Weir Group Company Information
- 6.8.2 Weir Group Business Overview
- 6.8.3 Weir Group Knife Gate Valves Production, Value and Gross Margin (2021-2026)
- 6.8.4 Weir Group Knife Gate Valves Product Portfolio
- 6.8.5 Weir Group Recent Developments
- 6.9 VAG
- 6.9.1 VAG Company Information
- 6.9.2 VAG Business Overview
- 6.9.3 VAG Knife Gate Valves Production, Value and Gross Margin (2021-2026)
- 6.9.4 VAG Knife Gate Valves Product Portfolio
- 6.9.5 VAG Recent Developments
- 6.10 Erhard GmbH
- 6.10.1 Erhard GmbH Company Information
- 6.10.2 Erhard GmbH Business Overview
- 6.10.3 Erhard GmbH Knife Gate Valves Production, Value and Gross Margin (2021-2026)
- 6.10.4 Erhard GmbH Knife Gate Valves Product Portfolio
- 6.10.5 Erhard GmbH Recent Developments
- 6.11 WEY Valve
- 6.11.1 WEY Valve Company Information
- 6.11.2 WEY Valve Business Overview
- 6.11.3 WEY Valve Knife Gate Valves Production, Value and Gross Margin (2021-2026)
- 6.11.4 WEY Valve Knife Gate Valves Product Portfolio
- 6.11.5 WEY Valve Recent Developments
- 6.12 Chisun Valve
- 6.12.1 Chisun Valve Company Information
- 6.12.2 Chisun Valve Business Overview
- 6.12.3 Chisun Valve Knife Gate Valves Production, Value and Gross Margin (2021-2026)
- 6.12.4 Chisun Valve Knife Gate Valves Product Portfolio
- 6.12.5 Chisun Valve Recent Developments
- 6.13 GEFA Processtechnik
- 6.13.1 GEFA Processtechnik Company Information
- 6.13.2 GEFA Processtechnik Business Overview
- 6.13.3 GEFA Processtechnik Knife Gate Valves Production, Value and Gross Margin (2021-2026)
- 6.13.4 GEFA Processtechnik Knife Gate Valves Product Portfolio
- 6.13.5 GEFA Processtechnik Recent Developments
- 6.14 Zhejiang Linuo Flow
- 6.14.1 Zhejiang Linuo Flow Company Information
- 6.14.2 Zhejiang Linuo Flow Business Overview
- 6.14.3 Zhejiang Linuo Flow Knife Gate Valves Production, Value and Gross Margin (2021-2026)
- 6.14.4 Zhejiang Linuo Flow Knife Gate Valves Product Portfolio
- 6.14.5 Zhejiang Linuo Flow Recent Developments
- 6.15 Valmet (Flowrox)
- 6.15.1 Valmet (Flowrox) Company Information
- 6.15.2 Valmet (Flowrox) Business Overview
- 6.15.3 Valmet (Flowrox) Knife Gate Valves Production, Value and Gross Margin (2021-2026)
- 6.15.4 Valmet (Flowrox) Knife Gate Valves Product Portfolio
- 6.15.5 Valmet (Flowrox) Recent Developments
- 6.16 Okumura Engineering
- 6.16.1 Okumura Engineering Company Information
- 6.16.2 Okumura Engineering Business Overview
- 6.16.3 Okumura Engineering Knife Gate Valves Production, Value and Gross Margin (2021-2026)
- 6.16.4 Okumura Engineering Knife Gate Valves Product Portfolio
- 6.16.5 Okumura Engineering Recent Developments
- 6.17 Tecofi
- 6.17.1 Tecofi Company Information
- 6.17.2 Tecofi Business Overview
- 6.17.3 Tecofi Knife Gate Valves Production, Value and Gross Margin (2021-2026)
- 6.17.4 Tecofi Knife Gate Valves Product Portfolio
- 6.17.5 Tecofi Recent Developments
- 6.18 Davis Valve
- 6.18.1 Davis Valve Company Information
- 6.18.2 Davis Valve Business Overview
- 6.18.3 Davis Valve Knife Gate Valves Production, Value and Gross Margin (2021-2026)
- 6.18.4 Davis Valve Knife Gate Valves Product Portfolio
- 6.18.5 Davis Valve Recent Developments
- 6.19 Supero Seiki
- 6.19.1 Supero Seiki Company Information
- 6.19.2 Supero Seiki Business Overview
- 6.19.3 Supero Seiki Knife Gate Valves Production, Value and Gross Margin (2021-2026)
- 6.19.4 Supero Seiki Knife Gate Valves Product Portfolio
- 6.19.5 Supero Seiki Recent Developments
- 6.20 Trueline Valve
- 6.20.1 Trueline Valve Company Information
- 6.20.2 Trueline Valve Business Overview
- 6.20.3 Trueline Valve Knife Gate Valves Production, Value and Gross Margin (2021-2026)
- 6.20.4 Trueline Valve Knife Gate Valves Product Portfolio
- 6.20.5 Trueline Valve Recent Developments
7 Global Knife Gate Valves Production by Region
- 7.1 Global Knife Gate Valves Production by Region: 2021 VS 2025 VS 2032
- 7.2 Global Knife Gate Valves Production by Region (2021-2032)
- 7.2.1 Global Knife Gate Valves Production by Region (2021-2026)
- 7.2.2 Global Knife Gate Valves Production Forecast by Region (2027-2032)
- 7.3 Global Knife Gate Valves Production by Region: 2021 VS 2025 VS 2032
- 7.4 Global Knife Gate Valves Production Value by Region (2021-2032)
- 7.4.1 Global Knife Gate Valves Production Value by Region (2021-2026)
- 7.4.2 Global Knife Gate Valves Production Value by Region (2027-2032)
- 7.5 Global Knife Gate Valves Market Price Analysis by Region (2021-2032)
- 7.6 Regional Production Value Trends (2021-2032)
- 7.6.1 North America Knife Gate Valves Production Value (2021-2032)
- 7.6.2 Europe Knife Gate Valves Production Value (2021-2032)
- 7.6.3 Asia-Pacific Knife Gate Valves Production Value (2021-2032)
- 7.6.4 South America Knife Gate Valves Production Value (2021-2032)
- 7.6.5 Middle East & Africa Knife Gate Valves Production Value (2021-2032)
8 Global Knife Gate Valves Consumption by Region
- 8.1 Global Knife Gate Valves Consumption by Region: 2021 VS 2025 VS 2032
- 8.2 Global Knife Gate Valves Consumption by Region (2021-2032)
- 8.2.1 Global Knife Gate Valves Consumption by Region (2021-2026)
- 8.2.2 Global Knife Gate Valves Consumption by Region (2027-2032)
- 8.3 North America
- 8.3.1 North America Knife Gate Valves Consumption Growth Rate by Country: 2021 VS 2025 VS 2032
- 8.3.2 North America Knife Gate Valves Consumption by Country (2021-2032)
- 8.3.3 U.S.
- 8.3.4 Canada
- 8.3.5 Mexico
- 8.4 Europe
- 8.4.1 Europe Knife Gate Valves Consumption Growth Rate by Country: 2021 VS 2025 VS 2032
- 8.4.2 Europe Knife Gate Valves Consumption by Country (2021-2032)
- 8.4.3 Germany
- 8.4.4 France
- 8.4.5 U.K.
- 8.4.6 Italy
- 8.4.7 Netherlands
- 8.5 Asia Pacific
- 8.5.1 Asia Pacific Knife Gate Valves Consumption Growth Rate by Country: 2021 VS 2025 VS 2032
- 8.5.2 Asia Pacific Knife Gate Valves Consumption by Country (2021-2032)
- 8.5.3 China
- 8.5.4 Japan
- 8.5.5 South Korea
- 8.5.6 Southeast Asia
- 8.5.7 India
- 8.5.8 Australia
- 8.6 South America
- 8.6.1 South America Knife Gate Valves Consumption Growth Rate by Country: 2021 VS 2025 VS 2032
- 8.6.2 South America Knife Gate Valves Consumption by Country (2021-2032)
- 8.6.3 Brazil
- 8.6.4 Argentina
- 8.6.5 Chile
- 8.6.6 Colombia
- 8.7 Middle East & Africa
- 8.7.1 Middle East & Africa Knife Gate Valves Consumption Growth Rate by Country: 2021 VS 2025 VS 2032
- 8.7.2 Middle East & Africa Knife Gate Valves Consumption by Country (2021-2032)
- 8.7.3 Egypt
- 8.7.4 South Africa
- 8.7.5 Israel
- 8.7.6 Türkiye
- 8.7.7 GCC Countries
9 Value Chain and Sales Channels Analysis
- 9.1 Knife Gate Valves Value Chain Analysis
- 9.1.1 Knife Gate Valves Key Raw Materials
- 9.1.2 Raw Materials Key Suppliers
- 9.1.3 Manufacturing Cost Structure
- 9.1.4 Knife Gate Valves Production Mode & Process
- 9.2 Knife Gate Valves Sales Channels Analysis
- 9.2.1 Direct Comparison with Distribution Share
- 9.2.2 Knife Gate Valves Distributors
- 9.2.3 Knife Gate Valves Customers
10 Concluding Insights
11 Appendix
- 11.1 Reasons for Doing This Study
- 11.2 Research Methodology
- 11.3 Research Process
- 11.4 Authors List of This Report
- 11.5 Data Source
- 11.5.1 Secondary Sources
- 11.5.2 Primary Sources
- 11.6 Disclaimer
GET THE RESEARCH
Choose your license.
Choose who needs access.
All options are for this report and research series.
PDF by email within 3–5 working days after payment confirmation.
Talk to an analyst